
BARE BOARD FABRICATION
The Complete Guide to PCB Manufacturing Processes
From production files to a tested bare board: understand each fabrication stage, the controls that matter, and the information needed for a reliable build.
PCB manufacturing turns a released circuit design into a physical network of copper conductors, insulating layers, and plated connections. The finished bare board must match both the electrical artwork and the mechanical drawing so that components can be assembled reliably.
This guide follows a conventional rigid multilayer PCB through fabrication. Double-sided boards omit the inner-layer build, while HDI, heavy-copper, RF, flexible, and rigid-flex constructions need different materials or additional operations. The production traveler for the approved construction determines the actual sequence.
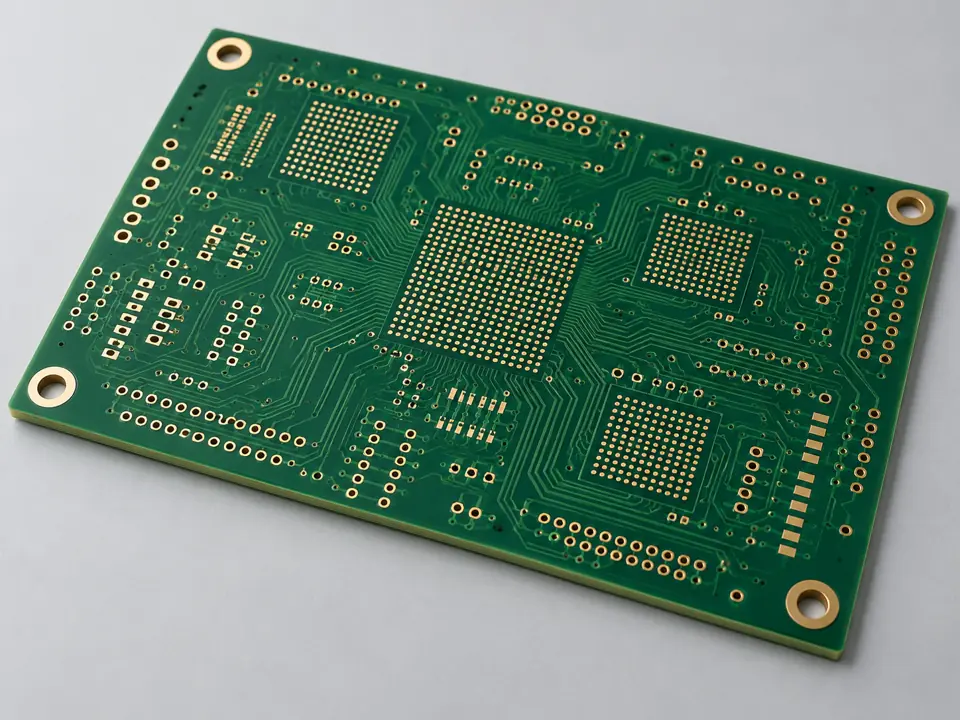
PCB Manufacturing Flow at a Glance
| Stage | What it produces | Main control |
|---|---|---|
| CAM and DFM review | A consistent, released production data set | Revision, dimensions, clearances, and stack-up |
| Inner-layer imaging and etching | Patterned copper cores | Conductor geometry and optical inspection |
| Lay-up and lamination | A bonded multilayer panel | Registration, dielectric build, and bonding |
| Drilling and metallization | Prepared and conductive interconnections | Hole position, wall preparation, and copper coverage |
| Outer-layer circuit formation | External traces, pads, and plated features | Finished geometry and plating thickness |
| Mask, finish, and legend | Protected circuitry and accessible connection areas | Openings, coating quality, and marking |
| Profiling, test, and inspection | Boards ready for delivery | Connectivity, dimensions, appearance, and traceability |
Some operations overlap or change order. For example, the relationship between panel plating, pattern plating, and etching depends on the selected process. A flowchart is a useful overview, not a universal recipe.
1. Release the Files and Complete Engineering Review
The first manufacturing task is to reconcile the data. Artwork, drill information, the fabrication drawing, and the stack-up must describe the same revision. If the outline in one file differs from another, production should not proceed on an assumption.
CAM engineers prepare the manufacturing data and panel layout. A design-for-manufacturing review checks whether the proposed geometry can be built with the chosen materials and process. Important items include conductor widths and gaps, drill-to-copper clearances, annular rings, solder-mask openings, copper-to-edge spacing, slots, and controlled-impedance structures.
- Fabrication data: Gerber or another agreed intelligent data format, drill files, and layer identification.
- Construction: layer sequence, material requirements, finished thickness, and copper requirements.
- Mechanical details: outline, plated and non-plated holes, slots, tolerances, and panelization.
- Acceptance: inspection criteria, electrical test, impedance targets, and required reports.
Engineering questions should be closed before material release. A requested artwork change needs approval and revision control; it should not silently alter the design intent.
2. Choose the Laminate, Copper, and Stack-Up
Many rigid boards use glass-reinforced epoxy laminate, commonly called FR-4. The material choice still requires more detail than that label: thermal behavior, dielectric properties, moisture performance, thickness, and compatibility with the intended assembly process all matter.
A multilayer stack commonly combines copper-clad cores, prepreg bonding sheets, and outer copper foil. Core thickness and prepreg construction influence the final dielectric spacing. Copper distribution also affects resin demand during lamination, so finished thickness cannot be estimated by simply adding nominal copper and glass dimensions.
Controlled impedance is reviewed with the fabricator using the actual stack-up, conductor geometry, and material data. An impedance target is not guaranteed by selecting a laminate name alone. Distinguish starting foil thickness from finished copper thickness, especially on outer layers that receive additional plating.
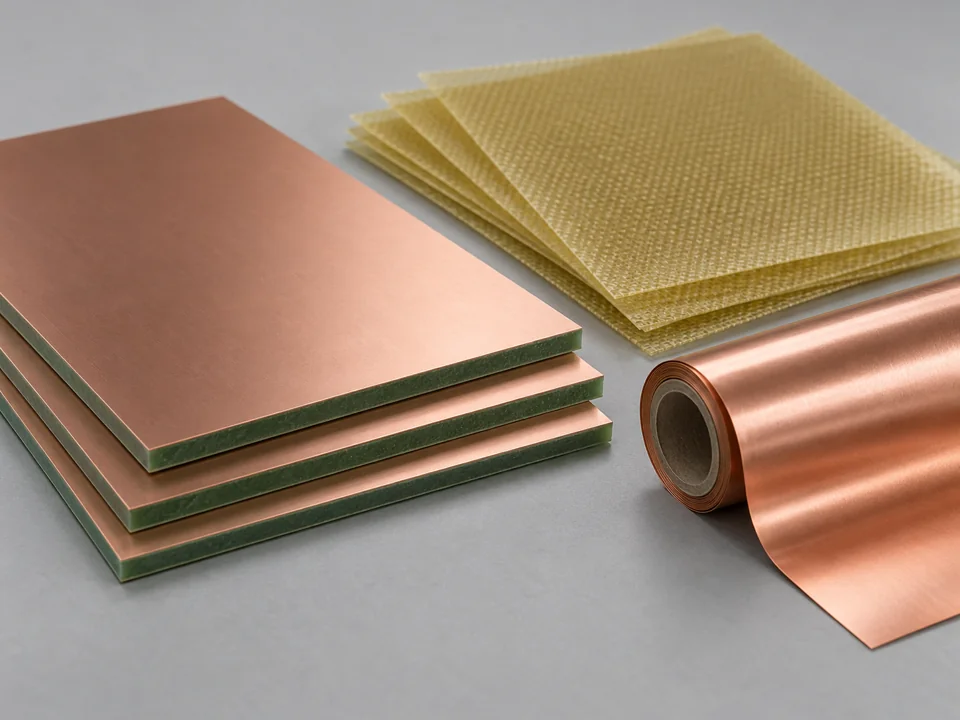
Incoming material identification and storage controls help maintain consistency. Panels are cut and prepared for subsequent imaging and registration operations.
3. Image, Etch, and Inspect the Inner Layers
The inner copper pattern is formed before the layers are buried inside the finished board. A photosensitive resist is applied to a prepared copper-clad core. Exposure, using suitable phototooling or direct imaging, and development define the protective pattern.
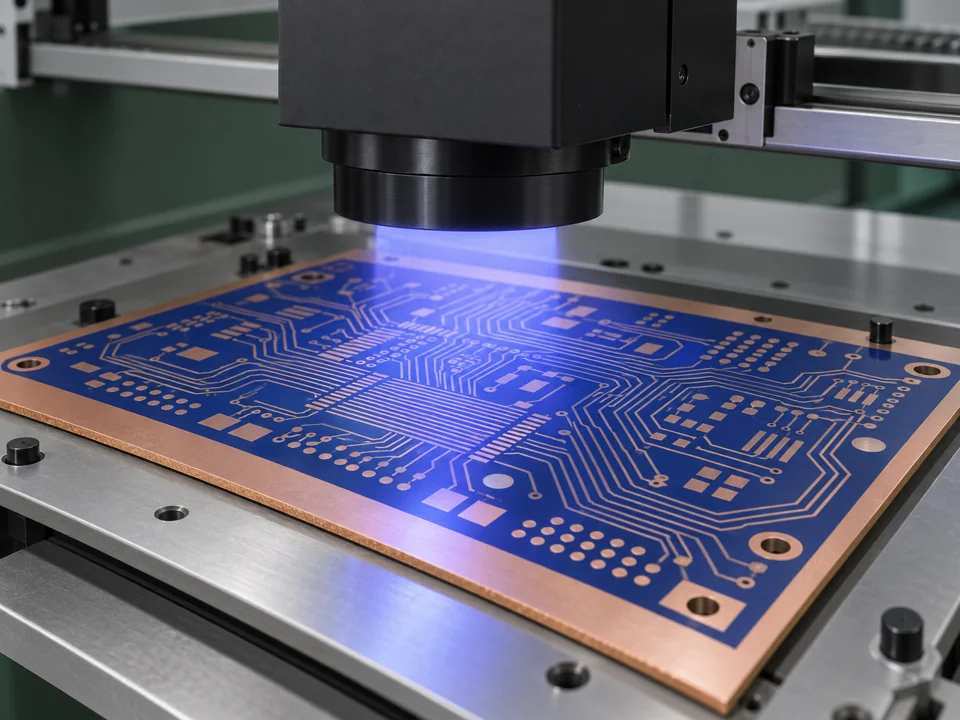
Etching removes the copper that is not required. The remaining resist is stripped, leaving the intended traces, planes, and clearances. Copper thickness, feature density, and etch conditions influence the final geometry; process compensation in the manufacturing artwork must still produce a board that meets the agreed requirements.
Inner-layer inspection is a critical hold point because those conductors will become inaccessible after pressing. Optical inspection compares visible patterns with reference data to identify suspect opens, bridges, or geometry errors. Detected features are reviewed before the cores are released for bonding.
A single-sided or double-sided board does not require this separate buried-layer stage.
4. Align the Layers and Laminate the Panel
Approved cores receive the appropriate surface preparation for bonding. Operators or automated systems arrange the cores, prepreg, and copper foil in the specified sequence using registration tooling. Reversing a core or using the wrong prepreg construction can invalidate an otherwise accurate circuit pattern.
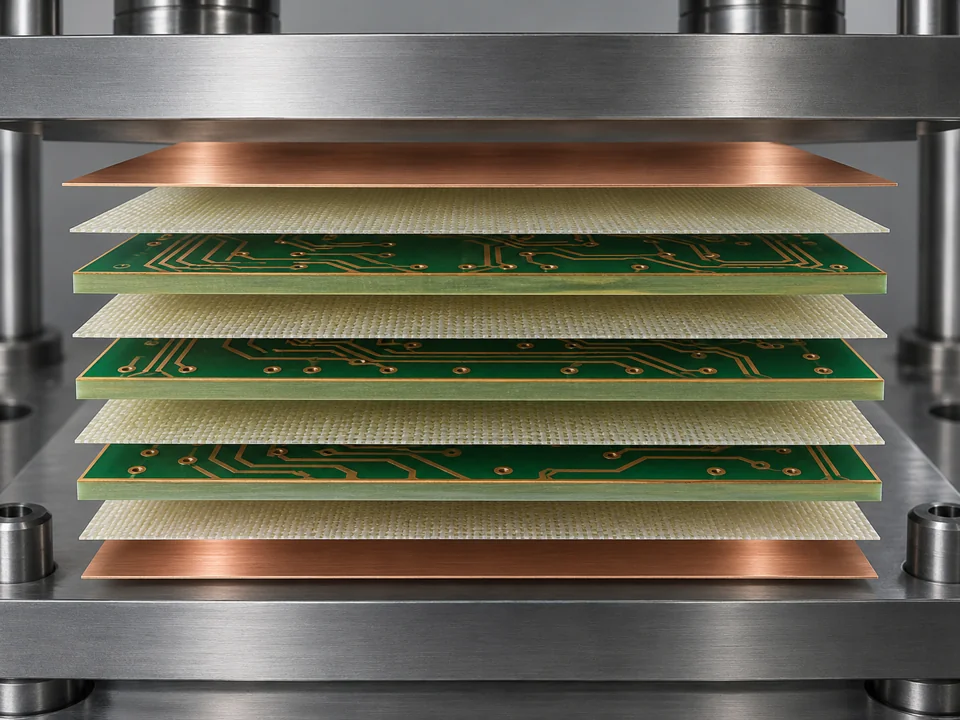
The lay-up is pressed under a qualified cycle. Resin flows and cures to bond the structure while pressure and process control help manage thickness and void formation. Temperature, pressure, time, and vacuum requirements depend on the laminate system and construction; they should not be copied from a generic online recipe.
After cooling and preparation, the panel continues to drilling. Registration and thickness checks help confirm that the bonded structure remains aligned with the production data. For multilayer PCB projects, agreeing the build before production reduces avoidable stack-up changes.
5. Drill the Features and Establish Conductive Hole Walls
Mechanical drilling creates many through-holes and vias. Laser processing is used for suitable microvia structures, rather than replacing every mechanical hole. Non-plated mounting holes are mechanical features and must remain distinct from plated electrical connections in the data and process plan.
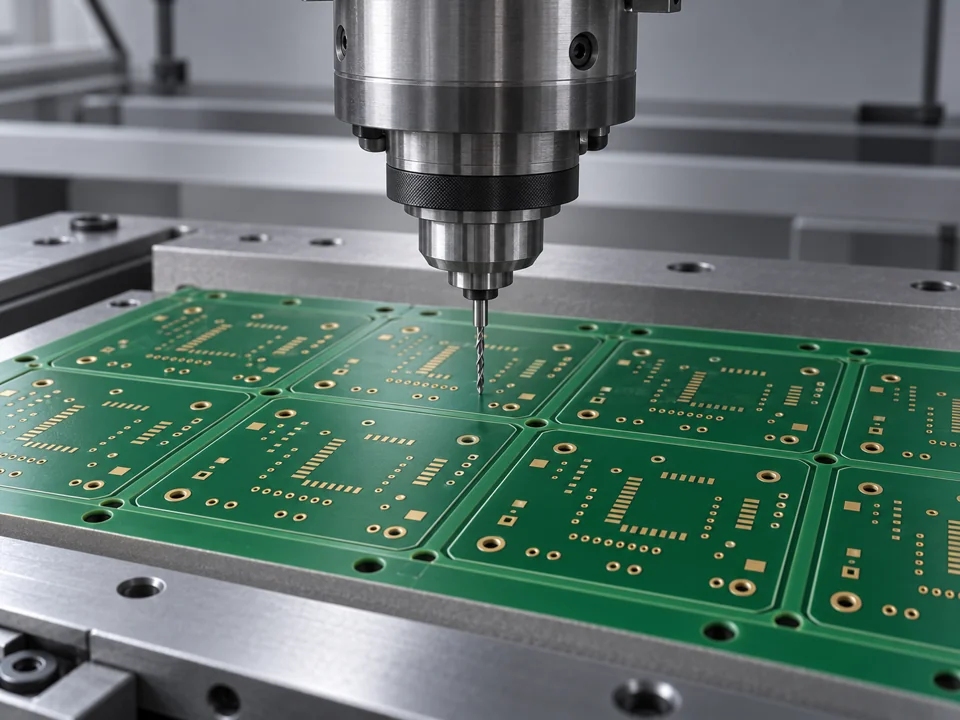
Drill position, tool condition, stack height, entry and backing materials, and the laminate influence hole quality. After drilling, appropriate cleaning and desmear prepare the walls and exposed inner-layer copper for metallization.
Because the dielectric wall is not naturally conductive, a qualified seed process establishes conductivity before electroplating builds copper. Electroless copper and direct metallization are examples of different approaches. The selected route must provide the required coverage and reliable connections to the intended layers.
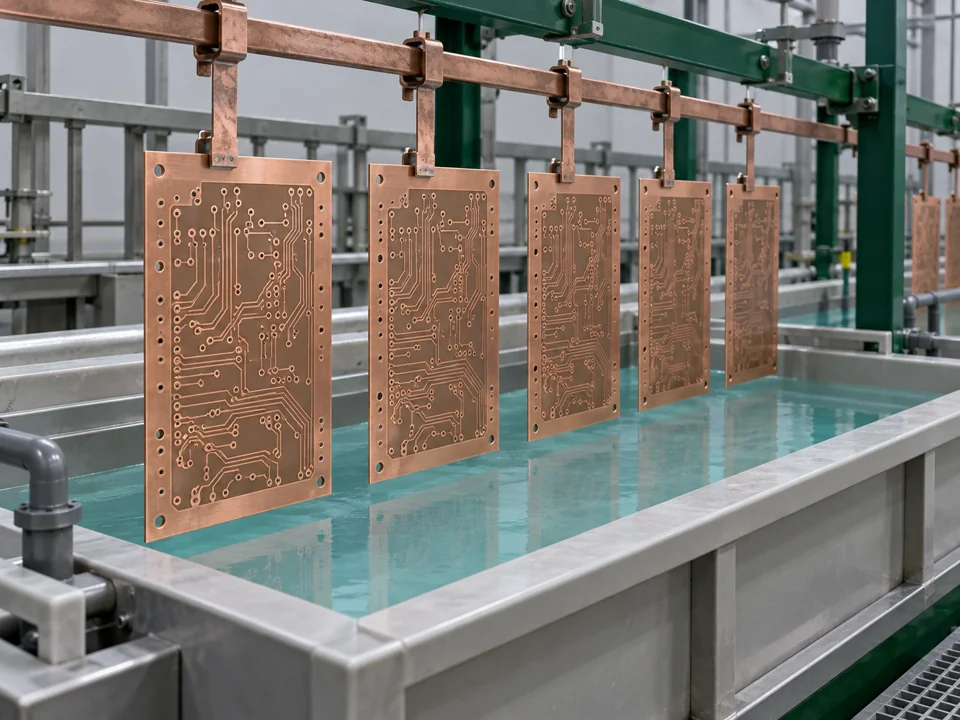
Finished hole diameter is different from the production drill diameter because plating reduces the opening. Hole size, aspect ratio, copper requirements, and tolerance should be reviewed together. Plating thickness is a controlled manufacturing characteristic, not something that can be confirmed by looking at the board surface.
6. Form the Outer-Layer Circuits
Outer layers need both circuit definition and the specified finished copper. In a common pattern-plating route, photoresist is imaged so the features to be plated remain exposed. Copper builds on those features and inside the prepared holes; an etch-resistant coating can protect the desired copper during later removal of the background foil.
Resist stripping, etching, and removal of the temporary etch protection complete the external conductor pattern. Other manufacturing routes use a different arrangement of plating and imaging. This is why describing outer-layer processing as simply repeating the inner-layer process is incomplete.
Inspection then checks accessible conductor geometry and suspected defects. Fine BGA escape routing, narrow gaps, and dense via fields need particular attention to the combined effects of imaging, etching, and copper build.
HDI PCBs may repeat lamination, laser drilling, via preparation, and plating to connect selected layer pairs. Stacked or staggered microvias need a design-specific build and qualification plan; adding more layers does not automatically make a board HDI.
7. Apply Solder Mask, Surface Finish, and Markings
Solder mask covers selected areas of the board while leaving specified connection sites accessible. A photoimageable coating is applied, imaged, developed, and cured using the qualified process. The mask artwork must align with pads and maintain the intended clearances.
Via treatment is a separate design decision. Tenting, plugging, and filling describe different results and should not be used interchangeably. An open via beside a solderable pad can behave differently during assembly from a filled and capped via-in-pad structure.
| Finish | What to review |
|---|---|
| ENIG | Flat pad surfaces, specified coating requirements, and compatibility with the connection process. |
| Lead-free HASL | Surface topography, pad geometry, and suitability for the assembly design. |
| OSP | Handling, storage, and the intended soldering sequence. |
| Immersion silver or tin | Application needs, storage conditions, and process compatibility. |
| Electrolytic gold | Contact usage and any wear, thickness, or selective-plating requirements. |
There is no universally best finish. Solderability, contact wear, flatness, storage, thermal exposure, and cost all contribute to the choice. The drawing should identify selective finish requirements where applicable.
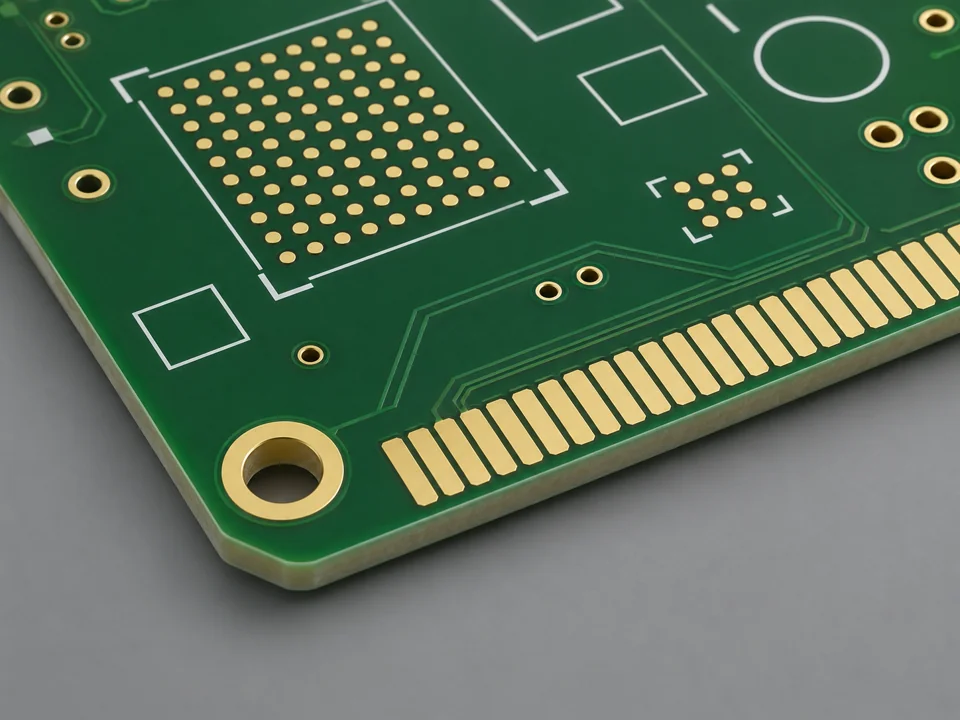
Legend markings add reference designators, orientation indicators, identification, and other agreed information. They must remain readable without contaminating solderable pads. The order of marking and finishing operations can vary with the process.
8. Profile, Test, and Verify the Finished Bare Board
Routing, scoring, or another suitable profiling method creates the final outline and separation features. Panel rails, breakaway tabs, keep-outs, and score depth should support the intended assembly and depanelization method. Routing dust and residues are removed before final inspection and packing.
| Control | What it evaluates | What it does not establish by itself |
|---|---|---|
| AOI and visual inspection | Accessible patterns, coatings, and visible defects | Every buried connection or complete electrical function |
| Bare-board electrical test | Connectivity and isolation against the agreed reference | Component operation or assembled product performance |
| Microsection analysis | Selected internal structures and plated features on a sample or coupon | Every feature on every delivered board |
| Impedance verification | Specified transmission-line structures, often using coupons | All aspects of signal integrity in the finished system |
| Dimensional inspection | Agreed holes, outlines, thicknesses, and tolerances | Electrical reliability under every service condition |
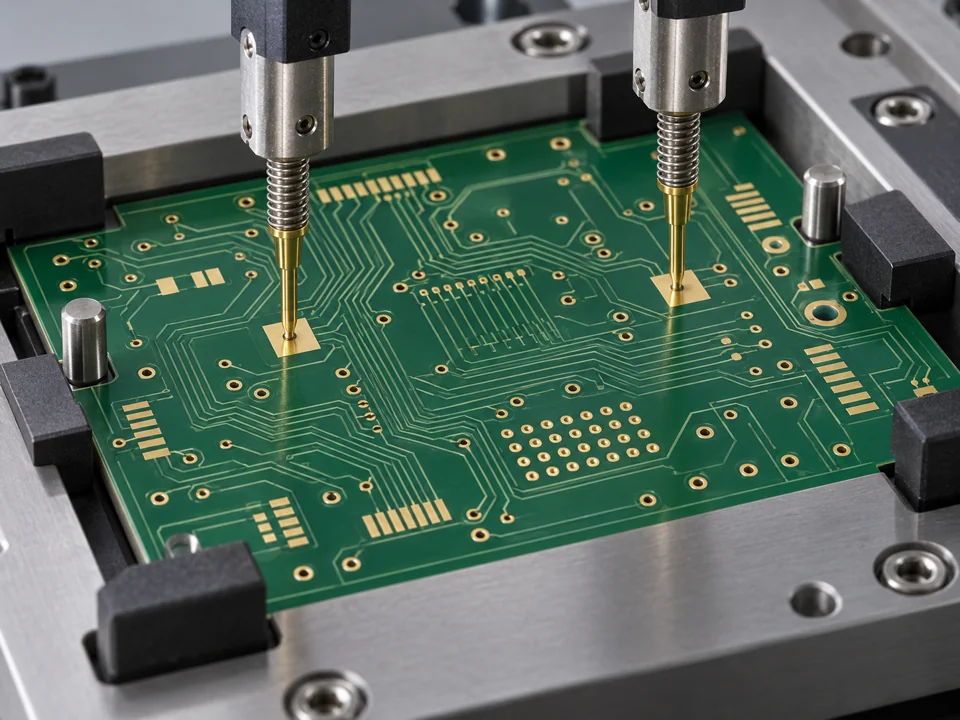
Flying-probe or fixture-based testing is selected according to access, volume, and the agreed test requirements. If an independent netlist is supplied, its role in data verification should be agreed. Microsections and other destructive checks use a defined sampling plan rather than being performed on every shipped board.
Final release reviews the required inspection results, identification, and documentation. Packaging protects surfaces and edges from contamination, abrasion, and mechanical damage. Storage and moisture precautions follow the chosen materials, finish, and delivery requirements.
What Drives PCB Cost and Lead Time?
Board area and order quantity matter, but process complexity often explains the difference between two similar-looking designs. Extra lamination cycles, unusual materials, tight registration, small holes, demanding copper structures, controlled-depth features, and added testing can require more operations or reduce manufacturing yield.
The most useful cost review asks which features are required by the application and which can be relaxed safely. Moving a via or adjusting a noncritical tolerance may simplify the process, but every change needs approval. A delivery date should be confirmed after the data, material availability, construction, and inspection scope are understood.
Prepare a Complete PCB Fabrication Inquiry
Send a revision-controlled data package with the artwork, drill data, drawing, layer stack, material requirements, finished copper, surface finish, solder mask, quantities, and target delivery. Identify critical tolerances and acceptance requirements explicitly. Include impedance structures and test documentation requirements where relevant.
If component assembly is included, also supply the BOM, placement data, assembly drawing, and any programming or functional-test requirements. For flexible constructions, see our separate flexible PCB manufacturing guide; for integrated rigid and flexible regions, review rigid-flex PCB requirements.
Discuss Your PCB Build with MV Circuit
Share your fabrication files and project priorities. Our team can review the board construction and coordinate PCB fabrication, component sourcing, assembly, and the agreed inspection scope.
Frequently Asked Questions
What is the difference between PCB fabrication and PCB assembly?
Fabrication makes the bare circuit board, including its conductors, holes, coatings, and outline. Assembly mounts and solders components and adds the inspection and testing required for the populated board.
Do double-sided PCBs need multilayer lamination?
A conventional double-sided board starts with copper on both faces of a dielectric core and does not need the separate inner-core lay-up used for a multilayer board. It can still require drilling, metallization, imaging, mask, finish, and testing.
Why are inner layers inspected before pressing?
After lamination, buried conductors cannot be inspected directly from the surface. Checking the patterned cores before bonding helps identify faults before additional manufacturing value is added.
Are all PCB holes plated?
No. Plated vias and through-holes provide electrical connections when specified. Mounting holes and other mechanical openings may be non-plated. The fabrication data must clearly distinguish them.
Is laser drilling used on every PCB?
No. Mechanical drilling remains suitable for many through-holes. Laser processing is selected for appropriate small blind-via structures and depends on the material and construction.
Why does finished hole size differ from drill size?
Copper deposited on the hole wall reduces the opening. Fabrication planning accounts for this difference so the delivered hole meets the specified finished diameter and tolerance.
Is ENIG always the best surface finish?
No. Finish selection depends on pad geometry, soldering, storage, contact use, and cost. A solderable pad and a wear-resistant connector contact can need different finishes.
Does electrical testing prove long-term reliability?
It checks the specified connectivity and isolation at the time of test. Thermal durability, material integrity, and application life require appropriate process controls and, where needed, additional qualification.
What changes when a PCB uses HDI construction?
Selected microvia connections can require repeated build-up, laser processing, preparation, and plating. The layer-pair connections and via structure determine the sequence and verification requirements.
How can I obtain a more accurate quotation?
Provide consistent fabrication files, a drawing, stack-up and material requirements, quantities, delivery expectations, and the test scope. Highlight unusual features before production planning begins.
Further technical reading: PCBAA: how PCBs are made and why HDI adds process cycles; Eurocircuits: outer-layer imaging; in-process inspection; microsection analysis.
This is a general fabrication guide. Process limits, acceptance criteria, sampling, and required documentation are confirmed for the specific order.